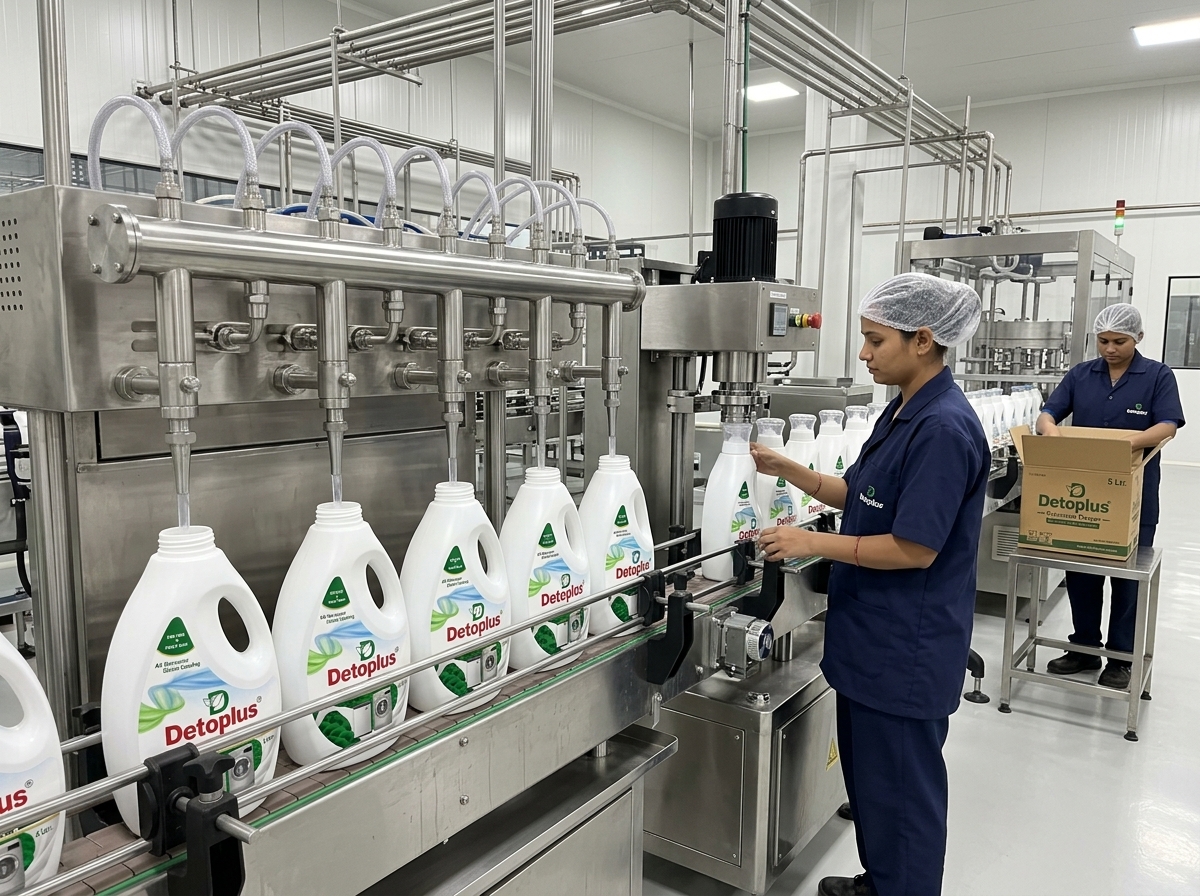
The 6-Stage Manufacturing Process
From verified raw materials to palletized container stuffing.
Raw Material Selection
Inspection of incoming surfactants (LABSA), soda ash, optical brighteners, and fragrances.
Batch Preparation
Computerized weighing and pre-dosing of active cleansing builders according to recipe sheets.
Mixing / Processing
High-shear homogenization for liquid detergents and ribbon blending for free-flowing powders.
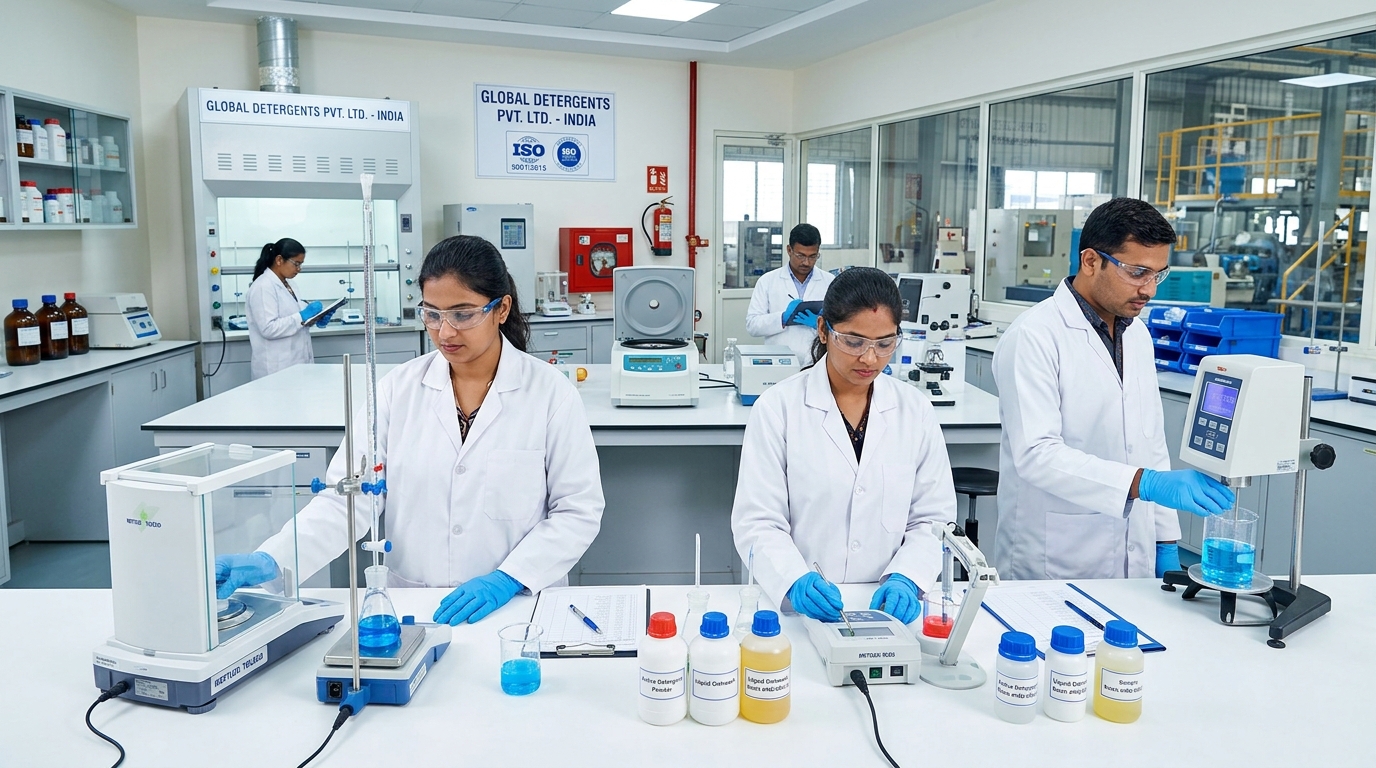
Quality Inspection
Intermediate laboratory verification for active matter %, pH balance, and viscosity.
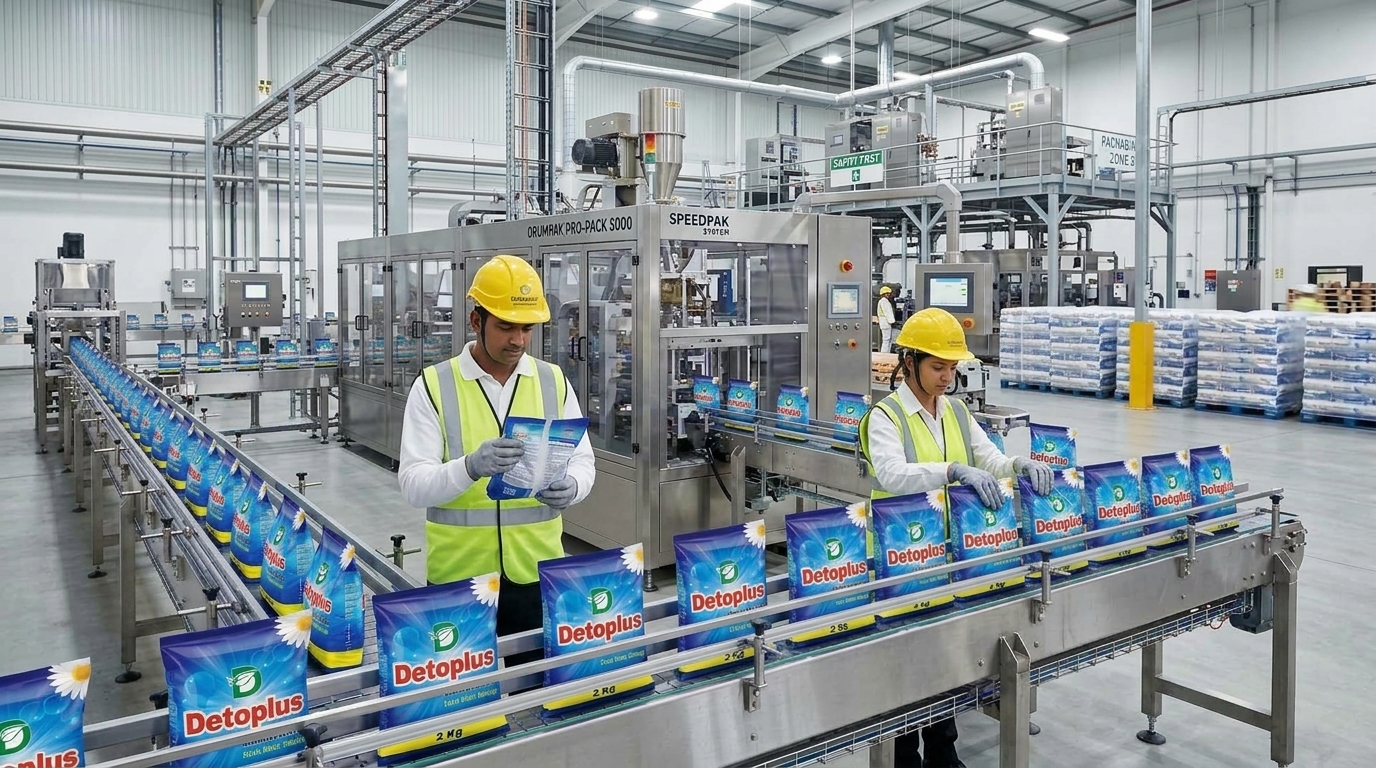
Packaging
Automated pouch form-fill-seal, bottle capping, leak detection, and master carton boxing.
Final Dispatch
Stretch-wrap palletization, container loading, and direct transit to ports or domestic hubs.
Quality Built Into Our Process
Disciplined quality assurance checks at each stage of manufacturing.
Raw Material Control
Suppliers are vetted; every raw material lot is sampled for purity, moisture %, and active ingredient concentration before batch charging.
Production Monitoring
Continuous monitoring of mixing speed, temperature, and dispersion ensures uniform granules and smooth liquid viscosity.
Batch Consistency
Strict master recipes guarantee that repeat orders exhibit identical fragrance, foam volume, and cleaning efficiency.
Packaging Inspection
Heat-seal tensile strength testing for pouches and drop/leak tests for plastic bottles to eliminate leakage during transit.
Final Quality Check
Final carton sampling, barcode scanning validation, and net weight checkweighing before pallet release.
Export Documentation
Each consignment is accompanied by an authentic Certificate of Analysis (COA) specifying verified parameters.
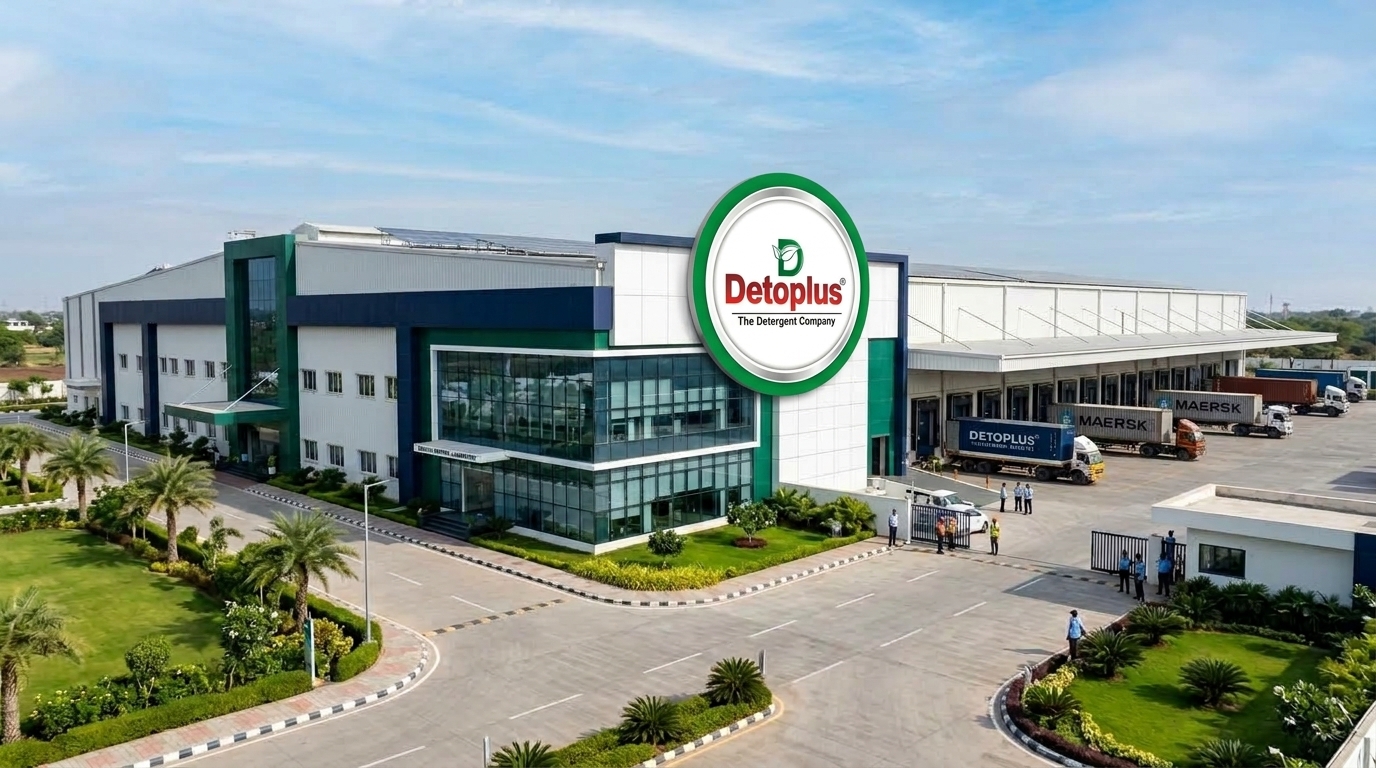
Want to Visit Our Factory in Surat, Gujarat?
We welcome prospective bulk buyers, distributor principals, and private-label brand managers for in-person factory visits or live video facility tours.